Cable Ferrule Crimp Guide for Clean Terminations

You've just stripped a flexible conductor for a control panel terminal. The copper strands fan out, one slips under the clamp, and the finished connection looks acceptable until vibration or repeated heating exposes the weakness. A proper cable ferrule crimp prevents that failure by forming the strands into a controlled termination that the terminal can clamp consistently.

Appearance is only the first check. A reliable termination depends on the conductor, ferrule, die profile, crimp position, tool condition, and verification method working together. The useful question isn't whether the sleeve looks compressed. It's whether the connection matches the applicable requirements and withstands the pull force expected for its conductor size.

Table of Contents

Why Cable Ferrules Exist and When They Apply

A stranded conductor can fail at the terminal even when the insulation and copper look undamaged. Individual strands may spread under a screw or spring clamp, creating uneven pressure and leaving the connection vulnerable to movement and oxidation. A ferrule holds the strands in a metal sleeve, presenting the terminal with a defined contact area rather than a loose bundle.

Ferrules entered widespread European practice in the latter half of the twentieth century as manufacturers sought to protect stranded copper conductors at terminal screws. That purpose remains practical: the sleeve controls the conductor mechanically before the terminal applies clamping force. The relevant practice is reflected in the DIN 46228 series, along with EN 60999-1 and EN 60352-2, as outlined in Phoenix Contact's standards guidance.

Match the conductor before choosing the sleeve

Select the ferrule from the conductor's cross-section, not from color alone. Insulated ferrules use standardized dimensions and color identification under DIN 46228-1. Ferrules intended for fine-stranded conductors require the tighter dimensional considerations associated with DIN 46228-4. The sleeve should accept the entire strand bundle without folding strands, shaving copper, or leaving empty space inside the barrel.

Conductor construction also affects the termination. Fine-stranded cable contains more individual strands, so insertion and compression need closer control. A tinned end presents another condition because solder can stiffen the conductor near the clamp. Treat it differently from clean, flexible copper prepared for a ferrule.

Practical rule: Use a ferrule when a stranded conductor enters a screw or spring terminal rated to accept ferrules, especially in control, instrumentation, safety-related, or vibration-exposed work. Confirm the terminal manufacturer's instructions before making the method standard.

Ferrule families commonly cover conductor cross-sections from 0.5 to 50 mm², roughly AWG 20 to 1/0. The range describes the product family, not the capacity of one crimp tool. Check the ferrule and die ratings against the actual conductor size, then verify the finished termination with the applicable pull-force requirement. A sleeve that fits physically can still be the wrong choice if its dimensions, conductor class, or crimp profile do not match the terminal and tool.

Choosing a Ferrule Crimp Tool for the Job

The tool profile determines how the sleeve deforms, how evenly it compresses the strands, and how well the finished end fits the terminal. Three families cover most panel and harness work: square-profile ratcheting tools, trapezoidal-profile tools, and four-indent pneumatic or heavy-duty ratcheting crimpers.

A square-profile ratcheting tool is the practical daily choice for many control-panel benches. It's quick, relatively affordable, and the completed ferrule has flat sides that seat neatly in many spring and screw terminals. Its limitation is coverage. A die window may handle a useful group of conductor sizes, but it won't automatically make the tool suitable for every ferrule in the drawer.

Trapezoidal-profile tools produce a compact, repeatable deformation favored in many European panel-building environments. They can give a clean termination that inserts smoothly into spring terminals, but the tool and ferrule still need to be matched. A neat shape doesn't compensate for a die that's outside its rated range.

Four-indent tools compress the sleeve from multiple directions and can produce a strong, near-round termination for fine-stranded cable and demanding harness work. They cost substantially more than everyday hand tools, so the investment makes sense where the work involves production volume, fine-stranded conductors, or documented pull-force requirements. For occasional panel repairs, their capability may be unnecessary.

Tool family Typical AWG / mm² range Crimp profile Relative cost Best fit for
Square-crimp ratcheting hand tool Depends on the marked die window Square Lower General control-panel wiring and service work
Trapezoidal-crimp ferrule tool Depends on the selected die Trapezoidal Moderate Repeatable European-style panel wiring and spring terminals
Four-indent pneumatic or ratcheting tool Depends on the ferrule and die set Four-indent, near-round Higher Fine-stranded cable, harness production, and documented quality programs

Check more than the profile. The important details are the rated conductor range, handle force at that range, die marking, ratchet completion, and calibration basis. A tool that merely says “automatic” or “self-adjusting” isn't automatically compliant with a particular ferrule standard. Look for documentation connecting the tool and ferrule system to the required dimensions and test method.

For sourcing, ATEK Distribution's tools and testing selection is one place to compare crimping and verification equipment alongside the rest of a project's electrical requirements. The tool still has to be selected against the conductor, ferrule, terminal, and acceptance procedure.

Preparing the Conductor and Ferrule

A pull test can expose a preparation error before the ferrule ever reaches the terminal. Measure strip length from the ferrule collar and barrel depth, then adjust the stripper so insulation finishes where the collar can support it. The copper should extend only slightly beyond the sleeve shoulder. Phoenix Contact's technical guidance limits conductor protrusion to no more than 1 mm in its validation workflow.

Use a sharp, correctly adjusted stripper. A nicked strand reduces the conductor's strength, even when the defect disappears inside the barrel. After stripping, trim fanned strands cleanly. Do not twist them tightly or push loose filaments back into position.

Build the fit in a controlled sequence

Match the ferrule to the conductor cross-section and the specified ferrule family. DIN 46228-1 assigns a color band to each cross-section, and adjacent sizes such as 1.0 mm² and 1.5 mm² can look alike in poor light. Select from a labeled strip magazine or tray, then confirm the printed size against the manufacturer's documentation. For two conductors, use a twin ferrule rated for that arrangement rather than forcing both wires into a standard sleeve.

Inspect the barrel before insertion. It must be clean, undamaged, and free of deformation. The conductor should enter straight until the insulation meets the inside of the collar. Keep the fit dry: lubricants and flux can affect the termination, while residue or visible oxidation can interfere with reliable contact.

A strand folded backward inside the barrel creates a hidden void or stress point that may reduce measured pull force. ATEK Distribution's wire and cable range can help source the conductor alongside the ferrule specification when the materials need to remain under one controlled purchasing process.

Crimping the Ferrule End to End

Insert the prepared conductor fully into the sleeve. Check the collar first. The insulation should approach the collar without being trapped beneath the metal barrel, and no stray strand should escape at the entry. If the conductor doesn't slide in straight, stop and correct the strip or ferrule selection before applying pressure.
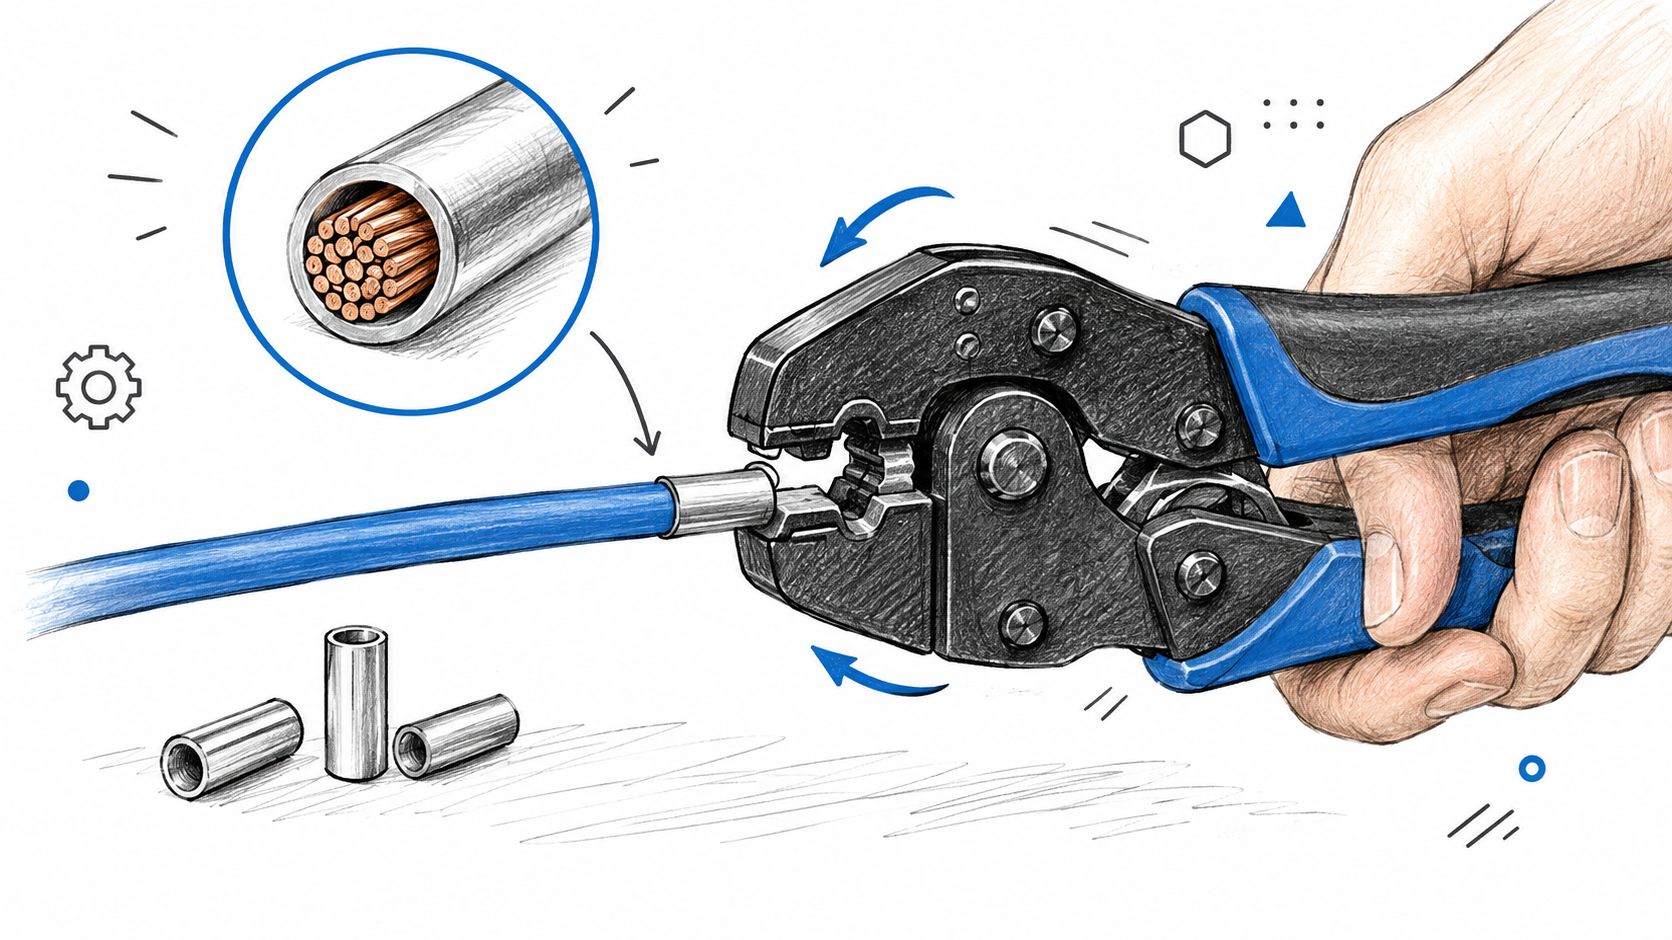
A hand using a specialized crimping tool to secure a metal ferrule onto the end of a blue electrical cable.

Place the ferrule in the die with the collar facing the correct direction and the sleeve centered in the rated crimp zone. The die should land close to the sleeve shoulder without crushing the plastic collar. Keep the crimp axis aligned with the conductor. A rotated or off-axis indentation can leave one side compressed while another side remains loose.

Close the tool through its complete cycle. With a ratcheting tool, don't reopen the handles halfway through and call the result finished. The ratchet exists to prevent partial compression, and the final release confirms that the designed stroke has been completed.

Control the compression across the sleeve

For larger sleeves or tools designed for multiple compression points, follow the manufacturer's sequence from the rear zone toward the front. The sleeve needs continuous support along its working length, not a single deep mark that leaves the rest of the barrel loose. Keep successive indentations in the same plane and re-square the ferrule before each compression when the tool requires repositioning.

A finished profile may be square, trapezoidal, or multi-indent depending on the tool. The profile should be even, with no fish-mouth opening, copper flash, split sleeve, or damaged collar. The wire should exit straight rather than bending sharply at the sleeve edge.

The Phoenix Contact crimping test guidance describes a validation approach in which the ferrule remains fixed under a target tensile load before the pull continues to failure. That is the standard to keep in mind while crimping. A clean shape is useful evidence, but it isn't the acceptance test.

A practical video demonstration can help operators see tool positioning and complete-stroke technique:

Inspecting the Crimp Against Pull Force

A pull test answers the question visual inspection can't. Does the conductor remain fixed in the ferrule under axial load, or does it slide before the connection reaches its expected strength? Standards-based ferrule practice ties quality to dimensions, tensile performance, and reliable contact formation, not to a crimp that merely looks symmetrical.

Published Weidmüller crimp tables provide these minimum pull-force values for selected conductor sizes: 10 N at 0.5 mm², 40 N at 1.5 mm², 60 N at 4 mm², 80 N at 6 mm², 100 N at 16 mm², 135 N at 25 mm², and 190 N at 35 mm². These values appear in Weidmüller's crimping documentation. Don't interpolate a value for an unlisted size and treat it as an approved requirement. Use the ferrule and tool manufacturer's table for the exact combination.

Conductor Size Minimum Pull Force (N) Typical Failure Mode Below Threshold
0.5 mm² 10 Conductor slips from an under-compressed sleeve
1.5 mm² 40 Strand bundle moves inside the ferrule
4 mm² 60 Partial compression or oversized die leaves a loose joint
6 mm² 80 Sleeve deformation doesn't retain the conductor
16 mm² 100 Incomplete compression or poor die match
25 mm² 135 Large-conductor sleeve slips or fractures at the exit
35 mm² 190 Insufficient full-length compression or tool mismatch

Run the test as a controlled check

Clamp the ferrule or its test fixture without damaging the sleeve. Apply axial force with a pull gauge or load cell, hold the target load for the specified duration, and then continue at the prescribed rate until failure. The technical workflow described by Phoenix Contact holds the target load for 60 seconds and then increases the pull speed to about 25 mm/min. A passing connection remains fixed at the target load, while the conductor shouldn't pull out before the intended failure condition.

Visual inspection still matters. Check that the collar is intact, the indentation is symmetric, insulation isn't trapped beneath the barrel, and no copper has been shaved or pushed outside the sleeve. A crimp that looks excellent but falls below the applicable pull-force requirement is scrap.

NASA ultrasonic inspection research also shows why production teams shouldn't rely on appearance alone. One NASA study detected under-crimped terminations at a 97% detection rate, 93 of 96 samples, with a 1% false-call rate, 1 of 96, when ultrasonic transmission exceeded a threshold amplitude. The NASA report also connects ultrasonic amplitude changes with destructive pull-test outcomes. For routine bench work, calibrated tooling and destructive sampling may be sufficient. For higher-volume production, ultrasonic verification can add a non-destructive quality control layer.

Mistakes That Fail the Crimp Every Time

The failures that cause trouble are usually small and repeatable. A wrong strip length, mismatched die, or incomplete tool stroke can produce a termination that passes a casual visual check while failing under pull or vibration.
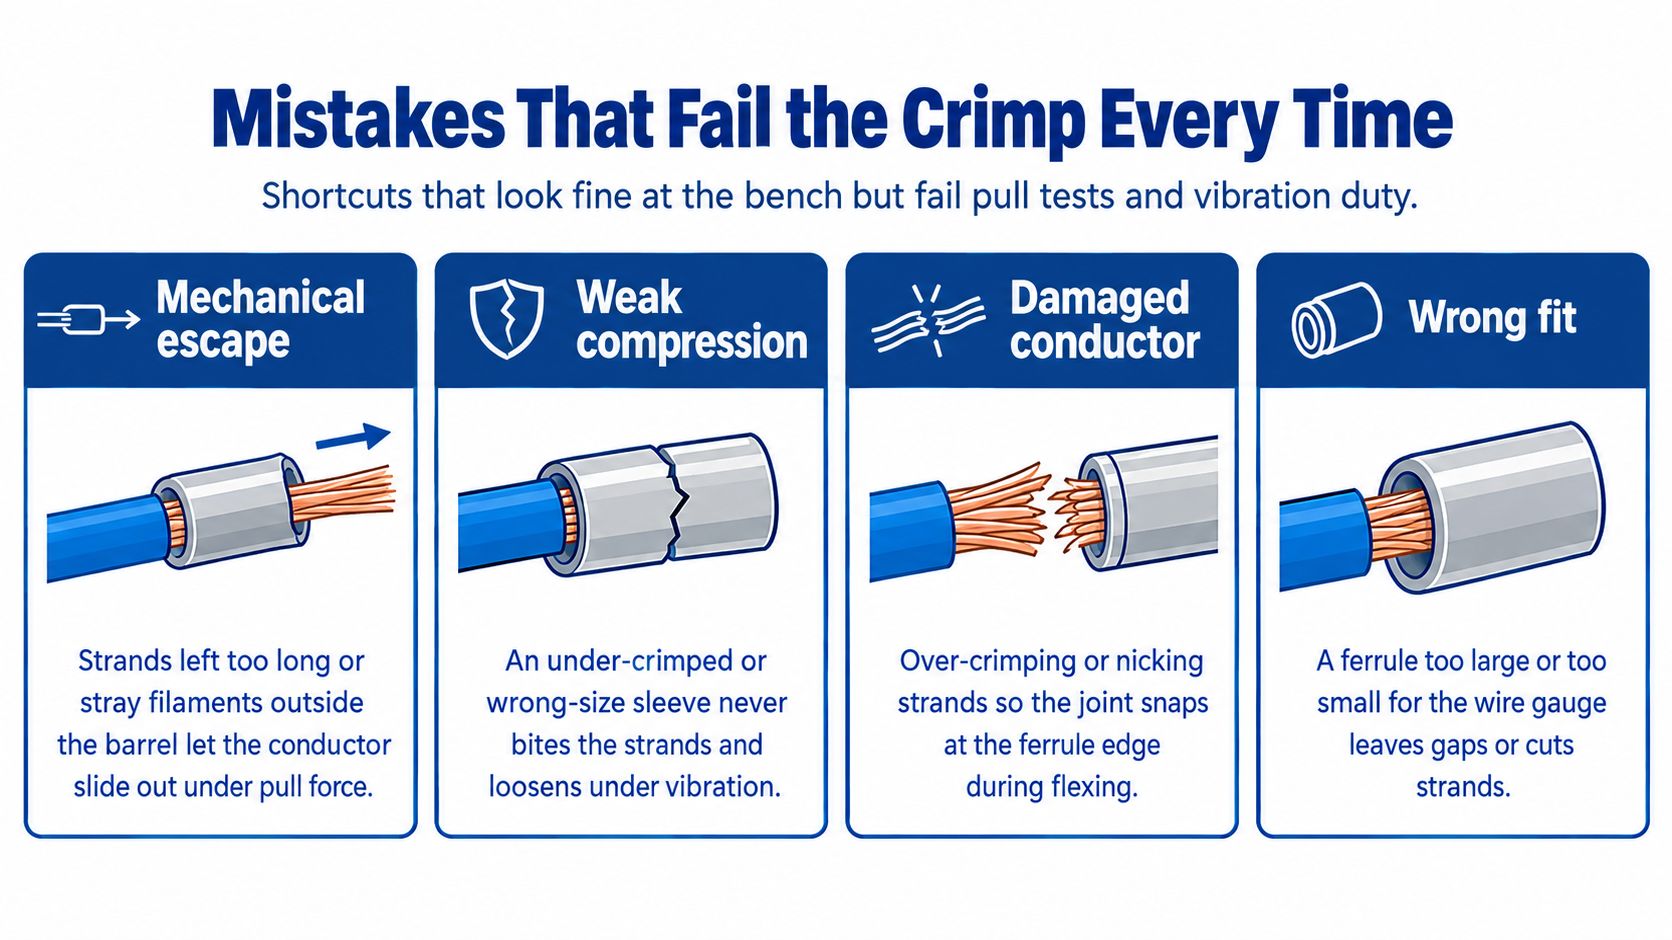
An educational infographic illustrating four common crimping mistakes that lead to electrical connection failures.

Start with the mechanical escape paths

A short strip leaves a gap between the conductor end and the sleeve nose. That reduces the supported length and gives the strand bundle room to move. An excessively long strip exposes copper beyond the sleeve, which can interfere with terminal clearance and create an avoidable electrical hazard.

A mismatched die fails in two directions. An oversized die leaves the strands insufficiently compressed, while an undersized die can shave strands, crush the collar, or force copper out of the barrel. The correct die window is the one specified for the ferrule and conductor, not the closest opening that happens to accept the part.

Look for compression defects

Rotated indents, partial handle closure, and skipped compression zones leave gaps in the sleeve. Those gaps may allow movement and oxidation, increasing contact resistance over service life. A complete ratchet cycle and consistent die alignment remove much of that operator variation.

Tool condition matters just as much. Worn jaws, loose pivot pins, contamination in the die, or a ratchet mechanism that no longer completes its designed stroke can produce weak crimps even when the operator follows the sequence. Inspect the tool when a pull test fails. Replacing the ferrule without correcting the tool only repeats the defect.

Protect the conductor before it enters the sleeve

A dull stripper can nick strands. Insulation left under the barrel prevents the sleeve from gripping the intended copper length. Pre-tinned conductors bring solder creep and a rigid transition into a termination designed for flexible strands. Tinning isn't a substitute for a ferrule in a screw or spring terminal.

A two-wire shortcut isn't a standard termination. If two conductors need to enter one terminal, use a correctly specified twin ferrule and matching tool, or use an approved terminal arrangement.

A standard ferrule isn't a license to cram two wires into one sleeve. The barrel, collar, conductor combination, and tool must be designed for that configuration. If the terminal needs separate conductors, use separate ferrules or an approved bridging method. If the application calls for a ring, fork, or specialized connector, use that termination instead of forcing a ferrule into the wrong hardware.

When a Ferrule Is the Right Termination

The decision starts with the terminal, not the tool drawer. A ferrule is usually the right choice when a stranded conductor enters a screw or spring-clamp terminal rated for ferrules, especially where vibration, repeated service, or consistent insertion matters. The terminal manufacturer's instructions remain decisive because some terminals specify a particular ferrule profile, conductor class, or insertion length.

Ferrules are particularly useful for flexible control wiring and fine-stranded conductors because they contain the strands before clamping. They're also preferable to solder-tinning a stranded end. Tinning creates a rigid section that can fracture or deform under clamp pressure, while a correctly selected ferrule preserves a controlled mechanical termination.

Use the application as the decision filter

Do not add a ferrule automatically to every electrical connection. A ring or fork terminal is the proper choice for a stud or screw designed for that lug. A direct termination may be specified for a connector that doesn't accept ferrules. A PCB pigtail may need a connector or soldered joint designed for that board, not a ferrule selected from a panel-wiring kit.

Termination Method Best Application Standards Reference Key Limitation
Insulated ferrule Stranded conductor in an approved screw or spring terminal DIN 46228-1, EN 60999-1 Must match conductor size, terminal, and tool
Fine-stranded ferrule Flexible or fine-stranded conductor requiring controlled clamping DIN 46228-4, EN 60352-2 More sensitive to sleeve and tooling mismatch
Twin ferrule Two conductors entering a terminal approved for that arrangement Applicable ferrule and terminal manufacturer requirements Requires a correctly sized twin sleeve and die
Ring or fork terminal Stud, busbar, or screw connection designed for a lug Equipment and terminal requirements Not a substitute for a ferrule in a cage or spring terminal
Direct conductor termination Terminal specifically rated for the conductor without a sleeve Terminal manufacturer's instructions Strands can splay if the terminal isn't designed for them
Soldered pigtail Board or component connection designed for solder Product and assembly requirements Not a replacement for a ferrule under a clamping terminal

Standards guidance links ferrule quality to dimensions, test methods, and tensile performance. The Weidmüller ferrule reference is useful when translating that logic into a selection decision, but the equipment maker's terminal data should control the final choice.

For buyers, ATEK Distribution's wire termination and supplies can help consolidate ferrules, crimp tools, wire, and related termination products around a defined specification. Confirm the conductor cross-section, ferrule family, crimp profile, terminal model, and inspection requirement before placing a project-wide order.

A dependable cable ferrule crimp program is simple to state: match the sleeve, prepare clean copper, complete the correct die cycle, inspect the geometry, and verify pull performance against the applicable table. ATEK Distribution supplies electrical products and procurement support for contractors, industrial teams, facilities, utilities, and government buyers, including sourcing help for wire, cable, tools, and termination requirements. Visit ATEK Distribution to discuss the ferrules, crimping equipment, and project documentation your installation needs.
Supply Chain Reliability: How Service-First Organizations Keep Critical Operations Running

A supply chain is not just a logistics function anymore. It is the invisible engine that keeps hospitals functioning, factories running, utilities stable, and governments operational. When it works smoothly, nobody notices. But when it fails, everything stops. That is the harsh reality modern organizations are dealing with.

In critical industries, even a small delay can create a chain reaction of problems. A missing part can shut down production. A delayed medical supply can postpone a surgery. A late shipment of essential components can stall infrastructure repairs. This is why supply chain reliability has shifted from a back-office concern to a boardroom-level priority.

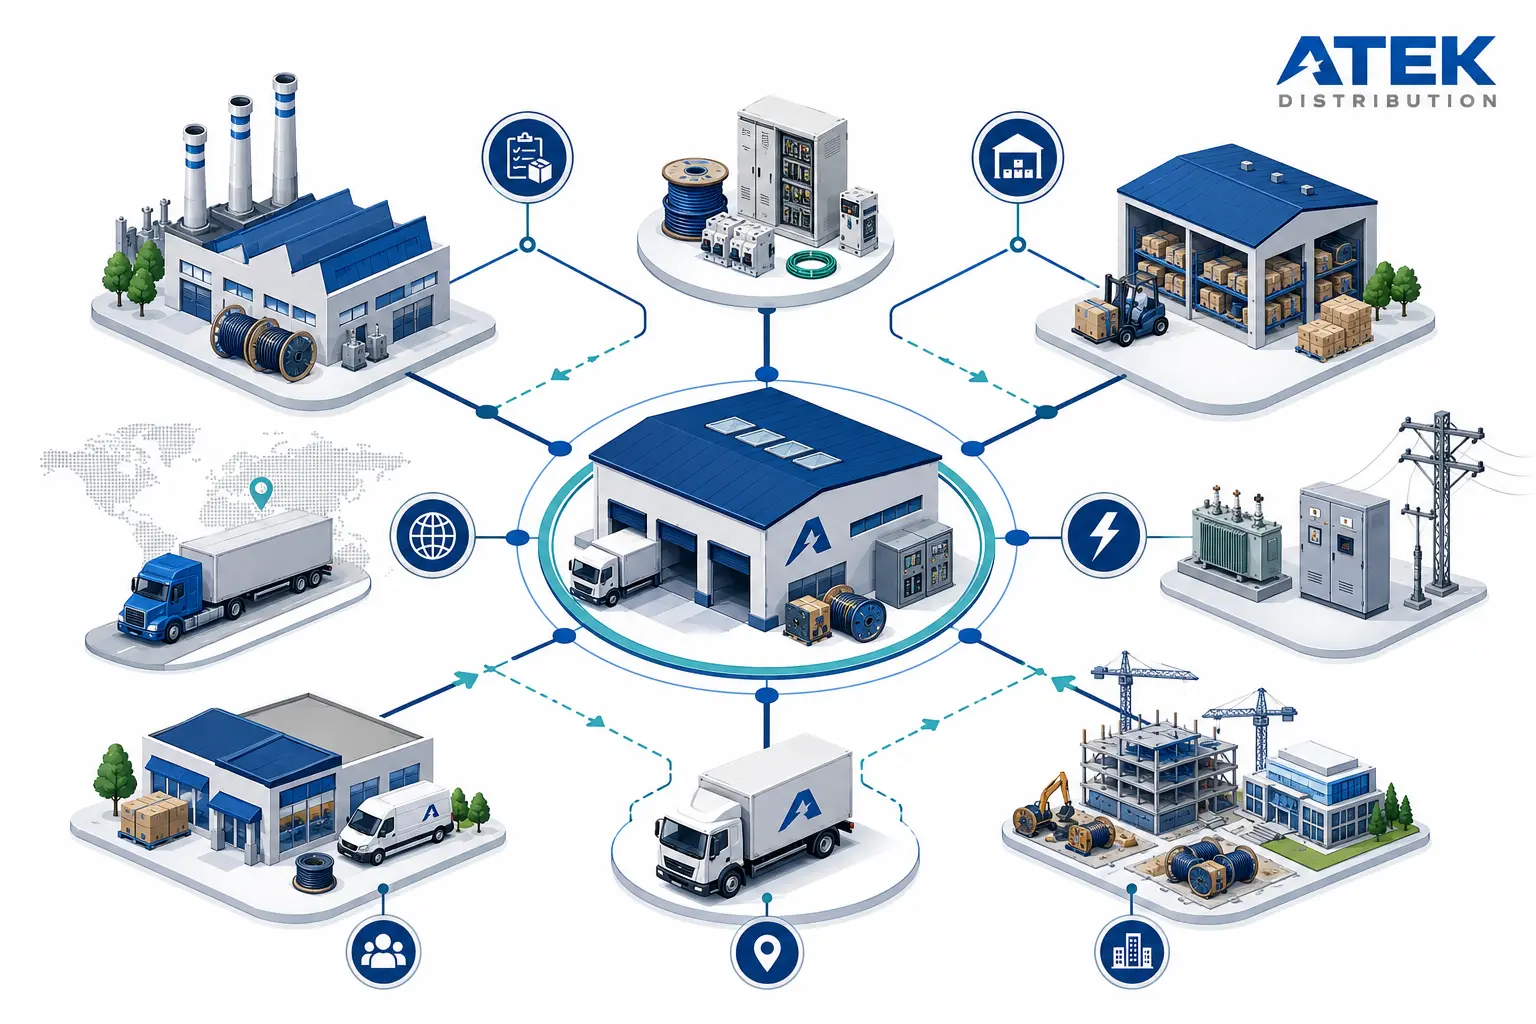
supply chain reliability network connecting warehouses factories and logistics partners

Why Supply Chain Reliability Matters Today

Shift from Price to Reliability

Not long ago, procurement decisions were dominated by one factor: price. The lowest bidder often won the contract. But that mindset is changing fast. Organizations are now realizing that the cheapest supplier is not always the most cost-effective partner in the long run.

Today, reliability has become the real currency of procurement. Companies are no longer asking only "How much does it cost?" They are asking deeper operational questions about execution, consistency, and risk handling. Can the vendor deliver under pressure? Can they respond quickly when something goes wrong? Can they anticipate disruptions before they happen?

This shift is especially visible in industries like healthcare, manufacturing, and energy, where downtime is extremely expensive. A slightly higher-priced but reliable supplier often results in significantly lower total operational cost compared to a cheaper but inconsistent one.

The Real Cost of Disruptions

Supply chain disruptions are rarely isolated events. They trigger ripple effects across entire operations. According to industry research such as Gartner insights on operational risk, disruptions can cost businesses between 6% and 10% of annual revenue depending on sector exposure. In high-risk industries, that number can be even higher.

But the real cost goes beyond financial loss. It includes:

  • Emergency procurement at inflated prices
  • Overtime labor costs due to delays
  • Production downtime and missed deadlines
  • Customer dissatisfaction and contract penalties
  • Reputational damage that affects future business

Most organizations underestimate these hidden costs until they experience them firsthand. A single missed delivery window can create a domino effect that takes days or even weeks to stabilize.

What Breaks Supply Chains in Real-World Operations

Inventory Visibility Gaps

One of the most common reasons supply chains fail is poor visibility. Many vendors still operate on outdated systems where inventory status is not updated in real time. As a result, customers only learn about shortages after placing orders.

This reactive model creates frustration and inefficiency. Instead of planning ahead, procurement teams are forced into constant firefighting mode. Modern supply chains require transparency, not surprises.

Single-Source Dependency Risks

Another major weakness is over-reliance on a single supplier or manufacturer. When that single source faces delays, shortages, or shutdowns, the entire chain collapses.

Organizations without backup sourcing strategies often find themselves stuck in long waiting cycles. A resilient supply chain always includes pre-qualified alternative suppliers who can step in when needed.

Communication Failures Between Stakeholders

Communication breakdown is one of the most underrated causes of supply chain disruption. In many cases, procurement teams, logistics providers, and end customers operate in silos.

This lack of coordination leads to missed updates, delayed responses, and confusion about order status. Reliable supply chains are built on structured communication systems where updates are proactive, not reactive.

What True Supply Chain Reliability Looks Like

Proactive Communication Systems

Reliable supply chain partners do not wait for customers to ask for updates. They actively communicate order status, risks, and changes in advance.

This includes:

  • Order confirmation updates
  • Shipment milestone tracking
  • Early warnings about delays
  • Transparent explanations when issues arise

Proactive communication transforms uncertainty into control. It builds trust and reduces operational stress on both sides.

Early Risk Detection Mechanisms

Strong supply chain systems continuously monitor risk factors such as supplier capacity, shipping delays, and regional disruptions. The goal is to identify problems before they reach the customer.

This requires a combination of technology and human expertise. Data systems can detect anomalies, but experienced professionals interpret what those signals mean in real operational terms. Together, they create a predictive rather than reactive supply chain model.

Fast Alternative Sourcing Capability

When a product becomes unavailable, speed matters more than anything else. Reliable suppliers maintain a network of pre-qualified alternative vendors who can be activated immediately.

This is not just about having contacts in a database. It is about having real operational relationships that allow fast substitution without compromising quality or compliance. ATEK Distribution maintains a network of trusted supply partners for exactly this reason — so customers never face a dead end when a critical product becomes unavailable.

End-to-End Accountability Model

Many supply chains fail not at the point of order placement, but after shipment. Once the product leaves the warehouse, accountability often disappears.

Service-first organizations operate differently. They remain responsible until the product is delivered, verified, and confirmed as usable by the customer. This closed-loop accountability ensures that no issue is left unresolved.

Industry Dependence on Reliable Supply Chains

Healthcare and Patient-Critical Operations

Healthcare is one of the most sensitive environments for supply chain failure. Hospitals depend on a constant flow of medical supplies, equipment, and consumables.

A delayed delivery is not just a logistical issue — it can affect patient treatment timelines and surgical schedules. In this sector, reliability directly impacts human life, making supply chain performance a clinical necessity rather than a business advantage.

Manufacturing, Utilities, and Infrastructure

Manufacturing plants operate on tightly scheduled production cycles. A missing component can halt entire assembly lines, causing financial losses and contractual delays. For plant and facility buyers, ATEK Distribution has a dedicated industrial electrical supply page.

Utilities and infrastructure providers face similar challenges. Whether it is power generation or water supply systems, downtime is not an option. These industries require uninterrupted access to critical components and maintenance supplies.

In both cases, supply chain reliability determines operational continuity.

A real-world example of this principle in action comes from ATEK Distribution, a Minneapolis-based electrical and MRO distributor serving government and enterprise customers. Facing the challenge of scaling their operations internationally, the company focused on building a more structured and visible digital supply presence. The results were significant — international active users of their platform grew by 143%. Their story was recognized by the U.S. International Trade Administration as a model of disciplined, service-first growth. It is a clear example of what happens when an organization prioritizes reliability and structure over shortcuts.

Reliability vs Price: The Procurement Reality

The assumption that lower price equals better value is one of the most expensive misconceptions in procurement strategy.

When evaluating total cost, organizations must consider:

  • Cost of delays
  • Emergency procurement expenses
  • Production losses
  • Administrative overhead
  • Customer relationship damage

A reliable supplier with slightly higher pricing often delivers significantly lower total cost of ownership. This is because operational stability eliminates hidden expenses that are not visible on invoices.

The smartest procurement teams now evaluate vendors based on consistency, responsiveness, transparency, expertise, and trustworthiness — rather than price alone.

Building a More Resilient Supply Chain System

Resilience is not built overnight. It requires intentional evaluation of vendors, processes, and communication systems.

Organizations should start by asking hard questions:

  • Do suppliers communicate proactively or reactively?
  • Are alternative sourcing options available when needed?
  • Is risk identification happening early enough to act on it?
  • Is accountability maintained beyond shipment?

If the answers reveal gaps, the supply chain is not resilient — it is fragile.

A resilient supply chain is not defined by the absence of problems, but by how quickly and effectively those problems are resolved.

Vendor Audit Checklist for Reliability

Before finalizing or continuing a supplier relationship, organizations should evaluate:

  • Consistency of on-time delivery performance
  • Quality and accuracy of fulfilled orders
  • Speed of issue resolution
  • Transparency in communication
  • Depth of sourcing network

These criteria separate transactional vendors from true supply chain partners.

Checking your current supplier against this list?

ATEK Distribution is a Service-Disabled Veteran-Owned Small Business (SDVOSB) electrical distributor in Minneapolis, Minnesota, with a GSA contract. Send us your bill of materials or parts list and we will quote it. Prefer the phone? Call 952-254-1205.

Conclusion

Supply chain reliability has become the backbone of modern operational success. It determines whether organizations can maintain continuity or face costly interruptions. In mission-critical industries, reliability is no longer optional — it is the foundation of performance, trust, and long-term sustainability.

Organizations that prioritize proactive communication, risk awareness, alternative sourcing, and accountability consistently outperform those that focus only on price. Over time, the difference compounds into stronger operations, fewer disruptions, and more predictable outcomes.

FREQUENTLY ASKED QUESTIONS

What is supply chain reliability?

Supply chain reliability refers to the consistent ability of a supplier to deliver the right products on time, in the correct quantity, and without disruption. It ensures smooth operational continuity across industries.

Why is supply chain reliability important?

It reduces downtime, prevents operational delays, and minimizes hidden costs like emergency procurement and production losses. It is especially critical in healthcare, manufacturing, and infrastructure sectors.

How do companies measure supply chain reliability?

Common metrics include on-time delivery rate, order accuracy, lead time consistency, and issue resolution speed. Advanced organizations also track communication responsiveness and risk detection efficiency.

What causes most supply chain failures?

Common causes include poor inventory visibility, over-reliance on single suppliers, weak communication systems, and lack of contingency planning.

Is reliability more important than price in procurement?

Yes, in most mission-critical industries. While price matters, reliability often determines total cost of ownership and long-term operational efficiency

Electrical Boxes: 8 Essential Components for Safe Installations

Electrical Boxes: Reliable Components for Every Electrical Installation

Electrical boxes are essential components in nearly every type of electrical system—whether it’s a small home project or a large commercial job. ATEK Distribution supplies a broad range of high-quality electrical boxes and accessory products from trusted manufacturers. Customers can order directly by calling ATEK or emailing
info@atekdistribution.com,
ensuring they receive dependable components at competitive pricing.

All electrical boxes and related installation components used in commercial and industrial environments must comply with applicable safety and performance standards, including requirements outlined by the

National Electrical Code (NEC).

.

Because electrical component pricing often fluctuates, ATEK encourages customers to lock in their pricing by contacting the team at (952) 254-1205 to place orders quickly and efficiently.


Why Choose ATEK for Electrical Boxes and Installation Products

ATEK Distribution has long-standing relationships with leading manufacturers, allowing customers to access the components they need without delays. These relationships also provide ATEK with advantages that many distributors lack—especially when it comes to navigating supply chain disruptions.

This strategic supplier network means you get consistent availability, fast delivery options, and strong support for both small and large-scale projects. Whether you’re outfitting a single circuit or equipping an entire facility, ATEK helps ensure the components arrive on time.


Common Electrical Box Accessories Used in Modern Installations

Electrical systems often require more than the box itself. A wide range of accessory components is used to support, organize, and protect wiring inside electrical enclosures. Some of the most commonly used accessories include:

1. Cable Connectors

These components secure electrical cables to the enclosure and prevent strain or wire damage. Popular types include wire nuts, twist-on connectors, and compression connectors.

2. Cable Clamps

Cable clamps hold wires firmly in place within the electrical boxes. They help prevent cables from being pulled loose or damaged during installation or maintenance.

3. Cable Ties

These simple but effective accessories help organize the wiring inside boxes and hubs, keeping installations neat and accessible.

4. Grounding Screws

Grounding screws provide a safe connection point between the circuit and the box. This ensures proper grounding and improves safety across the system.

5. Cable Sheaths and Conduit

Protective sheathing—such as flexible metal conduit (FMC), armored cable, or PVC—helps shield wires from moisture, abrasion, and environmental damage.

6. Circuit Breaker Panels

Panels distribute power across circuits. They include subpanels, load centers, and main breaker panels depending on system requirements.

7. Electrical Outlets and Switches

Outlets, switches, dimmers, and motion sensors provide power and control across various parts of a building.

8. Cable Support Systems

System components like cable trays, baskets, and ladders organize and support the wiring infrastructure used alongside electrical boxes.


How ATEK Supports Your Electrical Box Needs

ATEK does more than provide electrical boxes—they support engineers, contractors, and facilities with reliable parts, competitive pricing, and trustworthy supply chain coordination. With access to multiple manufacturers and a wide inventory, ATEK helps customers complete installations without delays.

Electrical Boxes for Modern Installations

EV Charging Stations: Available Today at ATEKDistribution.com

EV Charging Stations are now a critical infrastructure item that larger facilities and car dealerships among others have to have in order to be contenders in todays market. ATEK has the highest quality items from SemaConnect that range from home systems to high-end facilities needing high capacity for recharging fleets or customer vehicles.

As SemaConnect describes it:


Designed with You in Mind

We make installation easy from nuts to volts, with pre-assembled units that any licensed electrician can install. Designed from premium parts, SemaConnect charging stations deliver performance you can count on with the industry’s highest uptime and a design that’s electric.”…

ATEK has already sold to dealerships and facilities management groups to meet an ever-increasing demand for reliable, powerful EV charging stations. Call ATEK today or shop online and get started modernizing your locations.

Jeff Anderson named to Leadership Council of the National Small Business Association

Jeff Anderson Headshot

ATEK Distribution’s President, Jeff Anderson, was just named to the Leadership Council of the National Small Business Association (NSBA)! You can read about it here in this Press Release.

Jeff is a recognized leader in the small business community, and he’s looking forward to bringing his message to the people who need to hear it most: Congress.

And his message is small business advocacy, as he plans to take up issues such as tax reform, regulatory restraint, and access to capital for small businesses, especially those that embrace green technology.

ATEK is already doing the right thing by bringing green solutions in the form of supplying electrical, EV charging, and solar products. Responsibility to the environment has fallen on the private sector, and Jeff is leading that charge in more ways than one.

Power the Future with Solar and EV Solutions – Save Money & Go Green | ATEK Distribution

Solar and EV Solutions: Powering a Greener Future | ATEK Distribution

The global shift toward sustainability and carbon neutrality is no longer aspirational — it’s a necessity.
Organizations that fail to modernize their energy strategies risk falling behind on regulatory compliance, customer expectations,
and financial performance. ATEK Distribution is helping forward-thinking clients take the lead in this transition by delivering
next-generation solar and EV infrastructure solutions designed for long-term impact — not just quick installs.

Why Solar and EV Solutions Matter for a Sustainable Future

Why It Matters More Than Ever

🌞 Solar Is a Strategic Asset

Solar isn’t just about “going green” — it’s about enhancing financial resilience and unlocking strategic value:

  • Reduce energy costs and protect against utility rate volatility.
  • Qualify for federal, state, and local incentives that improve ROI.
  • Meet ESG (Environmental, Social, Governance) goals and public commitments to sustainability.

ATEK designs highly efficient solar systems tailored to each environment — from rooftops and parking structures
to large-scale commercial and government facilities. The result? Seamless integration, optimized performance,
and a measurable return on investment.

⚡ EV Infrastructure Is No Longer Optional — It’s Expected

The demand for electric vehicles (EVs) is growing exponentially. As EV adoption accelerates across consumer and fleet markets,
having robust EV charging infrastructure is a competitive necessity:

  • Attract and retain customers, tenants, and employees.
  • Comply with emerging local and federal mandates for EV-ready buildings.
  • Support fleet electrification for government and corporate operations.

ATEK delivers scalable, future-proof EV charging solutions designed for commercial, municipal, and public environments.
Whether building a single site or a distributed network, ATEK ensures systems are durable, compliant, and easy to manage.

⚡ Battery Storage Delivers More Than Backup Power

By integrating advanced battery storage with solar, ATEK helps organizations:

  • Minimize grid dependence and energy costs.
  • Enhance resilience during grid outages and extreme weather.
  • Enable load shifting and peak shaving to further optimize utility spend.
  • Future-proof energy infrastructure in alignment with evolving regulations.

Why ATEK? Partnership Over Product

Many providers focus on volume or lowest-cost bids—often at the expense of system performance and lifecycle value.
ATEK takes a different approach:

  • Engineering-first mindset: Every system is designed for maximum reliability, scalability, and ROI.
  • Veteran-owned with mission-critical experience: ATEK brings deep expertise in government, defense, and public-sector projects, where performance truly matters.
  • End-to-end support: From design and procurement to delivery and support, ATEK works side-by-side with clients throughout the entire lifecycle of each project.
  • Commitment to U.S. manufacturing: When required, ATEK prioritizes Made in the USA components to support domestic industry and compliance needs.

The Bottom Line: Build Energy Resilience Today

Investing in solar, EV infrastructure, and battery storage is no longer a future initiative — it’s a business and community imperative.

When you work with ATEK Distribution, you gain a trusted partner who understands the stakes and helps you navigate the complex technical,
financial, and regulatory landscape of sustainable power.

Don’t just install equipment — transform how you power your world.
ATEK will help you lead the way.
Contact us today to learn more.